Medical & Laboratory Storage Solutions
Explore our export-ready range of modular clinical cabinets, heavy-duty lab furniture, paraffin block compactors, and intelligent bedside units crafted for Melbourne health networks.
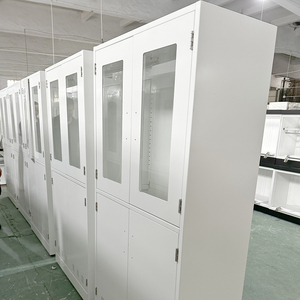
Lab Furniture Price School Laboratory Equipment Medical Cabinet
Heavy-duty electro-galvanized CRCA steel frame with chemical-resistant epoxy powder coating for educational and hospital testing labs.
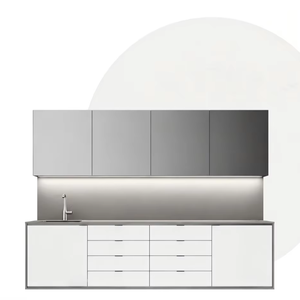
Professional Dental Medical Clinic Cabinet With Sink
Modular stainless steel clinical furniture equipped with integrated 304/316 grade seamless sink and touchless hygiene fixtures.
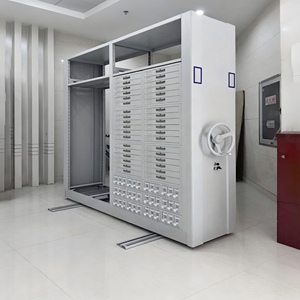
Microscope Slide & Paraffin Wax Block Storage Compactor
High-density mobile hand-push storage compactor system tailored for histology, pathology, and biobank specimen archives.
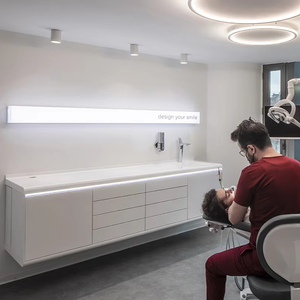
Custom Dental Cabinet Furniture With Modular Storage System
Ergonomic treatment room storage modules designed for seamless clinical workflow, instrument organization, and infection prevention.
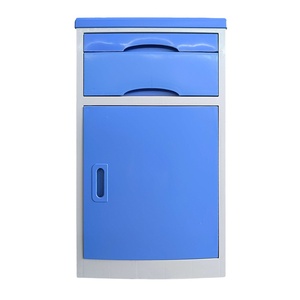
Wholesale Modern Plastic Hospital Bedside Table Cabinet
Multi-purpose ABS medical bedside cabinet featuring lightweight impact resistance, hidden towel hooks, and silent castors.
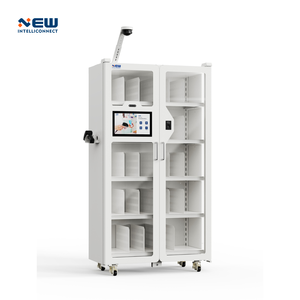
Invisible Intelligent Scanning Management Auxiliary Cabinet
Smart barcode & RFID tracking bedside cabinet for real-time inventory management of low-value clinical consumables and drugs.
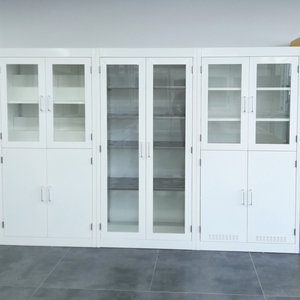
Steel Laboratory Chemical Storage Cabinet Epoxy Resin Coating
Corrosion-resistant steel chemical safety cabinet featuring anti-spill shelves, ventilation ports, and high-durability coating.
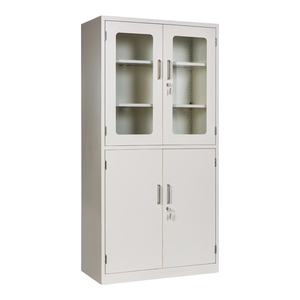
Modern Hospital Laboratory Steel Storage Cabinet Medicine & Biology
Versatile medical-grade steel storage unit designed for secure biology reagent, pharmaceutical, and clinical specimen storage.
Melbourne Healthcare Infrastructure & OEM/ODM Medical Storage Requirements
Melbourne’s medical ecosystem is currently experiencing one of the most dynamic expansion phases in the Southern Hemisphere. Major investments across the Parkville Biomedical Precinct, Monash Health Precinct, and regional health hubs managed under the Victorian Health Building Authority (VHBA) have established a benchmark for modern clinical architecture. In these high-intensity clinical environments, off-the-shelf storage furniture frequently fails to address the stringent requirements for infection control, space optimization, and workflow ergonomics.
As a established OEM/ODM medical storage cabinet manufacturer and exporter, our engineering team collaborates directly with Melbourne healthcare planners, hospital procurement teams, and biomedical facility managers. We bridge the gap between architectural layout requirements and factory-level precision fabrication. Whether equipping multi-bed general wards, high-containment pathology facilities, or private dental suites across suburban Melbourne, our medical-grade steel cabinetry complies fully with Australian healthcare building standards, including AS/NZS 4187 (Reprocessing of reusable medical devices) and AS 2243 (Safety in laboratories).
Information Gain Insight: Standard imported commercial cabinets often utilize basic 0.6mm cold-rolled steel with thin industrial powder coatings that degrade rapidly when exposed to hospital-grade disinfectants like sodium hypochlorite or hydrogen peroxide vapors. Our OEM/ODM medical cabinetry is constructed from 0.8mm to 1.2mm CRCA electro-galvanized steel finished with 80–100 micron anti-microbial epoxy-polyester resin coatings, preventing sub-surface oxidation for over 15 years in active clinical use.
Key Trends Driving Medical Storage Procurement in Victoria
- Infection Control Integration: Transition toward wall-mounted and modular floor-standing units with flush-welded joints, elimination of dust-collecting lip channels, and antibacterial surface treatments.
- Pathology Archival Density: Escalating demand for space-efficient paraffin block compactors and microscope slide cabinets capable of supporting heavy static load capacity within pathology laboratories in Clayton and Parkville.
- Digital Consumable Tracking: Integration of RFID and barcode scan auxiliary cabinets into bedside locker units to track low-value consumables automatically, reducing nursing inventory management hours by up to 30%.
OEM vs. ODM Manufacturing Engineering Capabilities
Our 35+ years of manufacturing background gives us the technical depth required to fulfill both Original Equipment Manufacturer (OEM) specifications provided by Australian distributors and Original Design Manufacturer (ODM) requests for bespoke clinical projects. Below is a technical comparison of our structural and functional customization capabilities tailored for medical facilities in Victoria.
| Engineering Parameter | OEM Standard Specification | ODM Customization Capability (Melbourne Projects) |
|---|---|---|
| Primary Construction Material | 0.8mm CRCA Steel / 304 Stainless Steel | 1.2mm Heavy Galvanized Steel / 316L Marine Stainless Steel |
| Surface Treatment & Coating | Electrostatic Epoxy Powder Coating (60–80μm) | Antibacterial Silver-Ion Epoxy Coating / Chemical Resistant Resin |
| Sink & Wet Area Integration | Standard Top-Mount Stainless Sink | Seamless Undermount 316 Stainless Sink with Hands-Free Tapware Sockets |
| Locking & Security Systems | Keyed Cam Lock / Mechanical Combination Lock | Invisible RFID Smart Reader / Electronic Scan Code / Centralized Access Control |
| Mobility & Base Configurations | Adjustable Leveling Feet or Castors | Seismic Base Anchor Brackets / Heavy-Duty 360° Medical Castors with Central Brakes |
| Infection Control Seals | Standard EPDM Door Gaskets | Hermetic Silicone Seals with Anti-Fungal Properties for Cleanrooms |
Localized Application Scenarios across Melbourne Healthcare Facilities
Healthcare infrastructure across Victoria presents diverse operational challenges. Our OEM/ODM manufacturing capability ensures that each storage cabinet line is optimized for its exact clinical location.
Facilities in areas like Box Hill, Frankston, and Brighton require modular dental cabinets featuring integrated sink units made from 304/316 grade stainless steel. These units facilitate strict instrument decontamination workflows while fitting compact room layouts.
High-throughput research and diagnostic centers demand specialized microscope slide and paraffin wax block storage compactors. Designed with high-density smooth-sliding tracks, these cabinets store hundreds of thousands of tissue specimens securely.
Modern inpatient rooms demand durable ABS plastic or steel hospital bedside lockers. Incorporating intelligent barcode scan auxiliary drawers allows nursing staff to log consumable usage automatically while giving patients easy access to personal belongings.
Academic research laboratories require specialized chemical storage cabinets finished with epoxy resin coating. Built-in fume extraction ports and double-walled steel thermal barriers safely store volatile biological reagents and chemicals.
Why Melbourne Healthcare Procurement Teams Partner With Us
Choosing an overseas manufacturing partner requires complete transparency, rigorous quality management, and reliable export logistics. Founded in 1987, our company operates state-of-the-art manufacturing facilities equipped with automated CNC laser cutting, robotic welding cells, and eco-friendly powder coating lines.
Key Institutional Credentials:
- Seven International Quality Certifications: Fully certified under ISO 13485 (Medical Devices Quality Management System), ISO 9001:2015, ISO 14001 (Environmental Management), ISO 45001 (Occupational Health & Safety), ISO 50001 (Energy Management), CE Certification, and compliance with IEC 60601-2-52 electrical safety standards for medical furniture.
- Export Shipping Logistics to Port of Melbourne: Proven shipping record supplying multi-unit container loads directly to the Port of Melbourne with full export clearance documentation, fumigation certificates, and customized protective wooden crate packaging.
- Strict Material Quality Assurance: Raw materials undergo salt spray testing (up to 500 hours without corrosion), load-bearing static testing on shelf supports (up to 150kg per shelf), and hinge cycle testing (exceeding 100,000 door openings).
- Turnkey OEM/ODM Engineering Support: Dedicated project managers assist with 2D layout drafting, 3D CAD modeling, sample prototyping, and localized hardware integration (such as Australian standard locks or electrical cutouts).
Frequently Asked Questions (FAQ)
Common questions from procurement officers, hospital architects, and medical equipment distributors serving Melbourne and Victoria.
What is the typical lead time for custom OEM/ODM cabinet orders to Melbourne?
Standard OEM production takes 20 to 25 days following engineering drawing sign-off. Direct sea freight from our export terminal to the Port of Melbourne typically takes an additional 14 to 18 days, allowing delivery within 5 to 6 weeks from initial order confirmation.
Do your medical storage cabinets comply with Australian infection control standards?
Yes. Our medical cabinetry is designed to align with AS/NZS 4187 guidelines. They feature seamless welds, non-porous antimicrobial powder coatings, chemical-resistant resin surfaces, and smooth interior corners to support strict cleaning routines.
Can you manufacture custom dimensions and color schemes for specific hospital branding?
Absolutely. Our ODM customization workflow allows precise adjustments to cabinet height, width, depth, internal shelving configurations, drawer counts, and color matching using standard RAL or Pantone color references.
What Minimum Order Quantity (MOQ) applies to OEM custom medical cabinetry?
We support both small-scale clinic fit-outs and multi-bed hospital development projects. While full container loads (20GP/40HQ) offer optimal freight efficiency, our minimum order quantity starts at just 10 units for custom OEM/ODM cabinet lines.
How are fragile items like sink units and slide compactors protected during ocean transit?
All cabinet units are wrapped in anti-static moisture barrier film, fitted with corner edge protectors, embedded in high-density EPE foam, and encased in ISPM-15 compliant export-grade wooden crates to prevent damage in transit.
How does the intelligent RFID scan code cabinet integrate into hospital management systems?
Our intelligent scan auxiliary cabinets support open API protocol integration. They interface directly with existing Hospital Information Systems (HIS) and ERP platforms over Wi-Fi/Ethernet to log item removal and generate restock alerts in real time.