Certified Medical Beds & Pressure Relief Support Surfaces
Engineered for intensive care units, long-term rehabilitation centers, and general hospital wards. Built to comply with international standards including ISO 13485, CE, and IEC 60601-2-52.
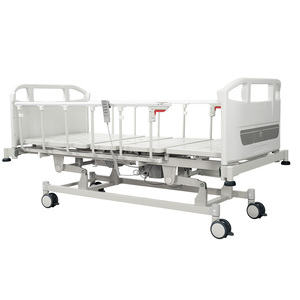
YXZ-C3 3-Function Electric ICU Bed with Medical Mattress
- ABS Tuck-Away Side Rails & Steel Deck
- High-Density Anti-Bedsore Foam Mattress
- ISO 13485 & CE Certified Platform
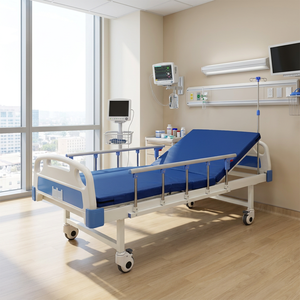
High-Quality Electric 2-Function Bed (5-Year Warranty)
- Back & Leg Rest Motorized Adjustment
- Waterproof Polyurethane Cover Mattress
- Heavy-Duty Steel Frame Structure
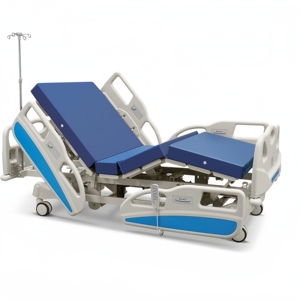
Cama Clinica 5-Function ICU Bed with Viscoelastic Mattress
- Trendelenburg & Reverse-Trendelenburg
- Multi-Zone Pressure Redistribution Core
- Central Locking Castor Control System
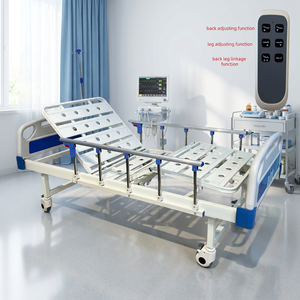
Dual-Function Electric Hospital Bed Direct Sales
- Ergonomic Patient Support Platform
- Flame-Retardant (CAL 133/BS 7177) Mattress
- Direct Export Factory Pricing
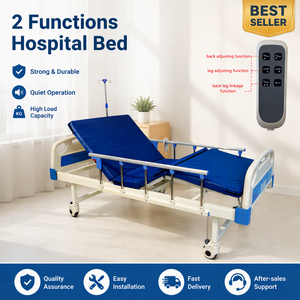
2-Function Electric Linkage Bed with Ward Mattress
- Synchronized Back-Leg Linkage Control
- Seamless Ultrasonic Welded Cushion Cover
- CE & ISO13485 Factory Wholesale
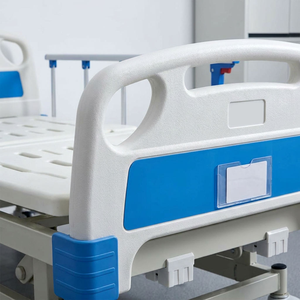
Medical-Grade 3-Function Bed with Steel Frame
- 1.2mm Heavy CRCA Powder-Coated Steel
- Anti-Bacterial Fluid-Proof Mattress
- Designed for High-Occupancy Wards
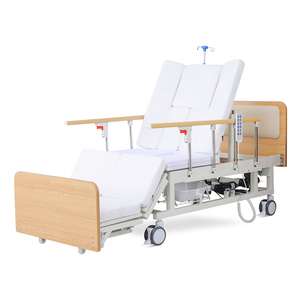
Automatic Lateral Turning Bed & Specialized Mattress
- Programmed Auto Lateral Tilt Mechanism
- Articulated Segmented Foam Core
- Ideal for Paralyzed & Elderly Care
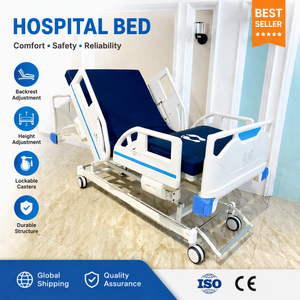
5-Function Height-Adjustable Bed with ICU Mattress
- Height Elevation & Full Cardiac Chair Mode
- Cold Polyurethane Molded Foam Base
- OEM Available with 5-Year Warranty
Technical Whitepaper: Engineering Next-Generation Hospital Mattresses & Clinical Support Surfaces
In modern clinical environments—spanning Intensive Care Units (ICUs), surgical recovery wards, and long-term care facilities—the medical mattress is far more than a basic bedding accessory. It functions as an active therapeutic medical device designed to mitigate deep tissue injury, prevent hospital-acquired pressure ulcers (HAPUs), regulate patient microclimates, and facilitate continuous caregiver workflows. As a premier China hospital mattress manufacturer and global exporter, our engineering philosophy fuses advanced biomechanical research with high-volume precision manufacturing.
Information Gain Insight: Capillary occlusion occurs when external interface pressure exceeds 32 mmHg over extended periods, obstructing localized blood flow and triggering tissue ischemia. Our engineered multi-zone viscoelastic support surfaces keep continuous interface pressures below 22 mmHg across critical anatomical bony prominences (sacrum, heels, and scapula).
1. Material Science & Multi-Density Core Architecture
The internal core of a medical-grade hospital mattress dictates its immersion, envelopment, and pressure-redistribution capabilities. Standard commercial polyurethane foams suffer from rapid indentation load deflection (ILD) degradation when exposed to repetitive cleaning chemicals and bodily fluids. Our manufacturing facility utilizes high-resilience (HR) cold-molded polyurethane combined with open-cell viscoelastic memory foam layers.
By engineering a gradient-density architecture—typically featuring a 32–38 kg/m³ supportive base layer paired with a 50–60 kg/m³ anatomical viscoelastic top contour—our hospital mattresses dynamically contour to the patient's body profile. This multi-zone cut design provides tailored resistance: softer support for lower-mass extremities (legs and feet) and firm, structured relief for high-mass core zones.
2. Infection Prevention & Fluid-Proof Barrier Fabrics
Cross-contamination control remains a primary benchmark for hospital procurement committees worldwide. A compromised mattress core serves as a reservoir for opportunistic pathogens, including Methicillin-resistant Staphylococcus aureus (MRSA) and Clostridioides difficile. Our export-grade hospital mattresses feature bi-elastic, polyurethane-coated barrier covers engineered with high hydrolytic stability.
Future Sourcing & Global Procurement Trends for Hospital Mattresses
As healthcare systems scale capacity and transition toward value-based patient care, hospital procurement directors, medical furniture importers, and ministry-of-health buyers are altering their evaluation metrics. Sourcing decisions have shifted from purely unit-cost evaluations to total cost of ownership (TCO), infection control compliance, environmental safety, and smart sensor integration.
Trend 1: Integration of IoT Sensors & Continuous Patient Monitoring
The next decade will mark a massive transition from passive foam mattresses to active, smart-sensing medical surfaces. Leading hospital bed manufacturers in China are integrating ultra-thin, flexible piezoelectric pressure sensor arrays directly beneath the top mattress cover. These arrays wirelessly communicate patient movement patterns, turn compliance, respiration rates, and early bed-exit warnings to central nursing stations, reducing caregiver burden and preventing patient falls.
Trend 2: Eco-Friendly Polyurethanes & Carbon-Neutral Supply Chains
With stringent global environmental initiatives (such as EU REACH, RoHS, and ESG corporate mandates), hospital procurement managers are demanding halogen-free, bio-based polyols in mattress production. Modern factories are replacing petroleum-derived polyols with natural castor bean and soybean derivatives, achieving zero-VOC off-gassing and complying with strict indoor air quality standards (Greenguard Gold certification) without compromising flame-retardant performance.
Trend 3: Strict Fire Retardancy Compliance (CAL 133 & BS 7177 Crib 5)
Fire safety standards for medical institutions vary drastically across international jurisdictions. B2B exporters must provide fully certified flame barrier technologies. In North America, compliance with California Technical Bulletin 133 (CAL 133) is mandatory for public occupancy facilities, while the UK and Commonwealth markets mandate BS 7177 Medium Hazard (Crib 5) testing. Our manufacturing operations utilize interliner barrier sleeves made from woven fiberglass or Kevlar aramid threads, ensuring full fire resistance without reliance on toxic chemical additives.
Frequently Asked Questions (FAQ) for Global Buyers & Importers
Key information for international hospital procurement teams, medical equipment distributors, and tender managers regarding sourcing, customization, and shipping logistics.
Ready to Partner with China's Premier Medical Mattress Exporter?
Contact our engineering sales team today to request complete product catalogs, technical data sheets (TDS), fire safety test reports, and wholesale OEM pricing quotes.