Featured Medication Distribution & Clinical Workstation Systems
Engineered for intense hospital operations, ICU care, and pharmacy distribution logistics. Built in certified ISO 13485 & CE facilities with heavy-gauge antimicrobial structural frames.
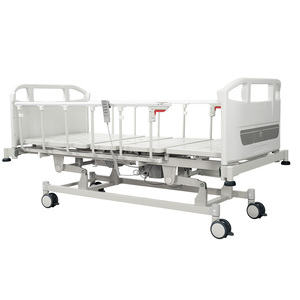
YXZ-C3(y302) 3-Function ICU Electric Distribution Station Bed
- High-grade ABS & cold-rolled steel structural frame
- 3-Function motorized control for rapid clinical response
- ISO certified antimicrobial wipe-down surfaces
- Central braking castors for smooth ward transit
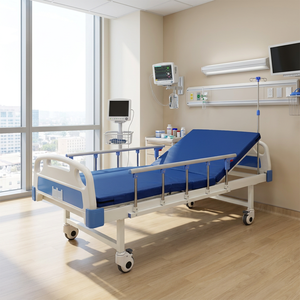
Bestselling High-Quality Electric 2-Function Ward Mobile Bed
- Reinforced chassis for high patient weight capacity
- Precision silent actuators for quiet ward movement
- Heavy-duty collision bumpers on all four corners
- Optimized for rapid medication delivery & bedside care
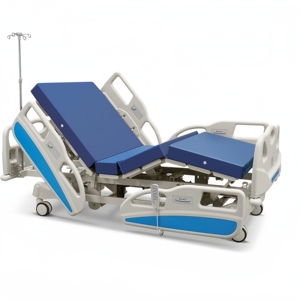
Cama Clinica Medical 5-Function ICU Electric Distribution Unit
- Full 5-function articulation: Hi-Lo, Trendelenburg, Back, Leg
- Integrated medical-grade high-density mattress included
- Side rail controls with integrated angle indicators
- Emergency CPR quick-release mechanism
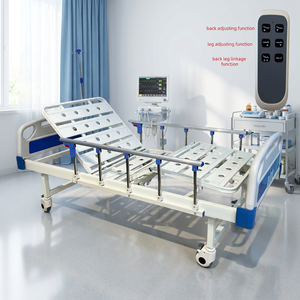
Dual-Function Electric Hospital Logistics & Patient Care Station
- Direct manufacturer pricing for hospital procurement tenders
- Dual-motor actuation with battery backup support
- Detachable head/foot boards for easy clearing
- Electrostatic epoxy powder coating against corrosion
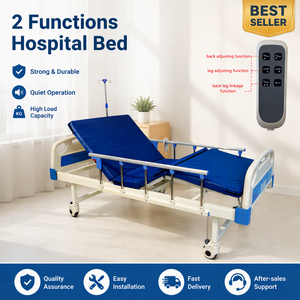
2-Function Electric Multifunction Medical Bed with Linkage Rails
- Synchronized back and leg linkage system for ergonomics
- Tuck-away collapsible safety side rails
- Heavy-duty 125mm medical casters with directional locks
- Wholesale bulk pricing available for project fulfillment
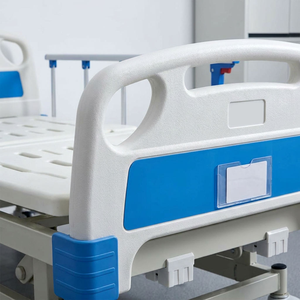
Medical Grade 3-Function Electric Bed for Hospital Wards
- 1.2mm thick structural steel tubing for structural rigidity
- Engineered for high-frequency daily nursing operations
- Smooth electric adjustment of height, head, and knee rests
- Seamless surface design prevents bio-burden accumulation
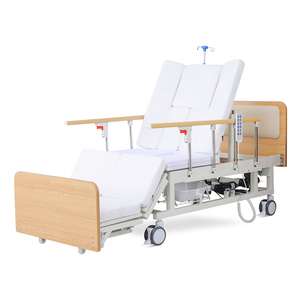
Multi-Functional Automatic Lateral Turning Nursing Distribution Bed
- Automated timed lateral tilt to prevent pressure ulcers
- Integrated commode function and dining/distribution tray
- Tailored for paralyzed, elderly, and long-term ICU patients
- Dual operational control: nurse master panel & remote
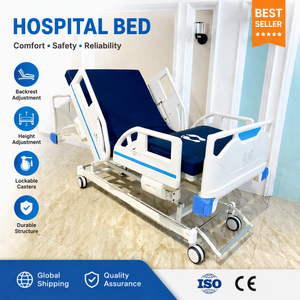
5-Function Electric Medical Distribution Bed with ABS Frame
- Full height-adjustable range from 450mm to 750mm
- Impact-resistant ABS molded head and foot panels
- CE & ISO 13485 fully compliant for global tenders
- Backed by factory 5-year structural framework support
Navigating Global Medication Distribution Cart Procurement
In modern clinical operations, medication errors remain one of the most critical safety challenges faced by hospital networks worldwide. Selecting the right medication distribution cart factory and exporter is no longer merely a procurement exercise in unit costs—it is a strategic decision that directly impacts patient outcomes, nursing efficiency, infection control compliance, and pharmacy chain-of-custody protocols.
| Evaluation Parameter | Tier 1 Export Standard (Gita Mediquip Class) | Standard Commercial Grade | Clinical Impact & Benefit |
|---|---|---|---|
| Structural Materials | 1.2mm Cold-Rolled Steel (CRCA) / ABS Engineering Polymers | 0.8mm Mild Steel or Reclaimed Plastics | Prevents structural sagging, extends lifespan to 10+ years under heavy clinical use. |
| Surface Antimicrobial Finish | Thermoset Epoxy Powder Coating + Silver-Ion Additives | Standard Paint Coating | Inhibits MRSA, E. coli, and pathogen bio-burden formation across touch points. |
| Mobility & Castor Assemblies | 125mm Precision German-engineered Central-Locking Silent Wheels | Standard Rubber Swivel Castors | Eliminates noise pollution in ICUs; enables effortless maneuverability over elevator thresholds. |
| Compliance & Certifications | CE, ISO 13485, ISO 9001, IEC 60601-2-52, ISO 14001 | Basic ISO 9001 Only | Guarantees compliance with international health authority audits and NABH/JCI standards. |
Future Procurement Trends for Hospital Supply Chains
Hospital procurement directors, B2B importers, and medical facility planners must align their purchasing strategies with emerging technological and operational shifts shaping clinical environments over the next decade.
1. Smart RFID & Biometric Access Control
Traditional key locks are rapidly being phased out in favor of electronic access control. Modern medication distribution carts incorporate RFID badge readers, biometric fingerprint scanners, and automated auto-locking timers. This enforces strict chain-of-custody for controlled substances and automatically logs every drawer access event into the hospital audit trail.
2. All-in-One Workstation Integration (COW)
The convergence of medication carts and Computer-on-Wheels (COW) workstations represents a major efficiency drive. Procurement teams are prioritizing carts with integrated lithium-iron-phosphate (LiFePO4) power systems, touch-screen monitor arms, and barcode scanners to enable real-time bedside barcode medication administration (BCMA).
3. Enhanced Ergonomics & Weight Reduction
Nurse fatigue and musculoskeletal strain are primary drivers of turnover in healthcare. Next-generation carts utilize hybrid structural designs—combining lightweight extruded aluminum pillars with high-impact ABS drawers—reducing push/pull force by up to 40% while preserving heavy load capacities.
4. Modular Cassette & Interchangeable Bin Architectures
Modern hospital pharmacies demand rapid replenishment workflows. Carts designed with removable exchange cassettes allow central pharmacy staff to pre-fill patient-specific medication trays and exchange entire cart sections in seconds, reducing turnaround time between shifts.
5. Green Manufacturing & SEER Compliance
International tender boards in Europe, the Middle East, and the Americas now require suppliers to demonstrate sustainable manufacturing. Importers prioritize factories certified under ISO 14001 (Environmental) and ISO 50001 (Energy Management), featuring zero-VOC powder coatings and recyclable materials.
Why Top Global Healthcare Networks Partner with Gita Mediquip
With over 35 years of dedicated specialization in medical furniture and clinical infrastructure, Gita Mediquip Pvt. Ltd. has established itself as an authoritative global manufacturer and exporter operating from Ahmedabad, Gujarat, India.
Rigorous International Certifications
Gita Mediquip operates under an audited integrated management system holding seven major international certifications: CE Certification, ISO 9001:2015 (Quality Management), ISO 13485 (Medical Devices), ISO 14001 (Environmental Management), ISO 45001 (Occupational Health & Safety), ISO 50001 (Energy Management), and IEC 60601-2-52 compliance for electrical safety.
The SEER Operating Philosophy
Every product engineered at Gita Mediquip adheres to the SEER benchmark: Socially Responsible (community workforce development), Ethically Operated (fair supplier pricing & full transparency), Environmentally Sustainable (waste reduction & green finishes), and Responsible Business (zero-compromise quality assurance).
Trusted by Premier Healthcare Institutions
Our products are deployed in leading multi-specialty hospital networks globally, including Apollo Hospitals, Zydus Hospitals, Manipal Hospitals, HCG Oncology Hospitals, SAL Hospital, Apex Heart Institute, Geetanjali Medical College & Hospital, and KD Hospital.
End-to-End OEM/ODM & Bulk Project Execution
From single-facility upgrades to massive 1,000-bed greenfield hospital builds, Gita Mediquip provides complete project management, modular custom fabrication, export container consolidation, and full technical documentation for international healthcare tenders.
Frequently Asked Questions for B2B Importers & Hospital Buyers
Key insights and operational clarity for procurement teams, hospital engineers, and medical equipment distributors worldwide.
What key factors should hospital procurement officers evaluate when selecting a medication distribution cart factory?
Procurement teams should evaluate five non-negotiable criteria: (1) Structural Integrity & Materials: Ensure the frame uses minimum 1.2mm CRCA steel or high-grade ABS engineering polymers; (2) Infection Control Finish: Verify ISO-certified antimicrobial powder coatings that resist harsh hospital disinfectant wipes; (3) Locking & Security Mechanics: Inspect central locking, digital keypad, or RFID access systems; (4) Castor Durability: Demand medical-grade, non-marking silent casters with central braking systems; and (5) International Compliance: Confirm CE and ISO 13485 certifications for medical device manufacturing.
Can Gita Mediquip customize medication carts and hospital equipment to meet specific hospital tender requirements?
Yes. As a direct manufacturer with complete in-house metal fabrication, powder coating, and assembly capabilities in Ahmedabad, India, Gita Mediquip provides comprehensive OEM/ODM customization. We can adjust drawer configurations, incorporate custom electronic lock mountings, modify dimensions, add IV pole accessories, and apply custom hospital brand color schemes.
What international export standards and certifications are provided for overseas shipments?
All export products are supplied with comprehensive technical documentation packages, including CE Declaration of Conformity, ISO 13485:2016 quality management documentation, Certificate of Origin, mill test certificates for raw steel, and factory inspection reports. Products are packed using ISPM-15 compliant export-grade wooden packaging to ensure safe ocean and air freight transit.
How do electric multi-function beds integrate into hospital medication distribution workflows?
Electric multi-function hospital beds (such as the 3-function and 5-function models featured above) serve as the vital endpoint of medication administration. Integrated side-rail controls, ergonomic height adjustment, and automatic lateral turning enable nurses to comfortably access patients during intravenous medication administration, decreasing the risk of accidental needle-stick injury and improving patient compliance during treatment cycles.
What is the typical lead time and shipping process for bulk international orders?
Standard manufacturing lead times for bulk orders (FCL - Full Container Loads) range between 15 to 30 business days depending on customization requirements. Shipments originate from major Indian ports (such as Mundra or Nhava Sheva), offering direct shipping routes to Europe, the Middle East, Southeast Asia, Africa, and the Americas. Dedicated logistics coordinators manage all export paperwork to facilitate seamless customs clearance.
Ready to Upgrade Your Hospital's Clinical Furniture & Distribution Infrastructure?
Connect directly with our engineering and international export division to request technical specifications, custom CAD drawings, and factory-direct quotation packages for your project.